How to weld new studs onto your tracks
XL Tracks are made from hot-rolled boron steel of the highest quality. Follow this instruction closely – it makes sure the track performs as it should after new studs have been welded on.
What you need
Heating
Propane or acetylene/oxygen.
Welding electrode
ESAB OK 48.00, 3.25 mm.
Pre-heating to 75 °C
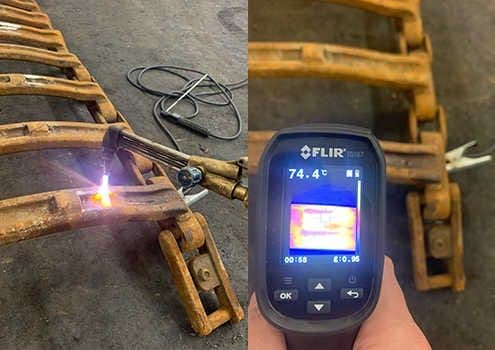
The track plate is heated to 75 °C before welding.
Dry tracks
At least 24 hours at room temperature after washing.
Step by step
Cleaning
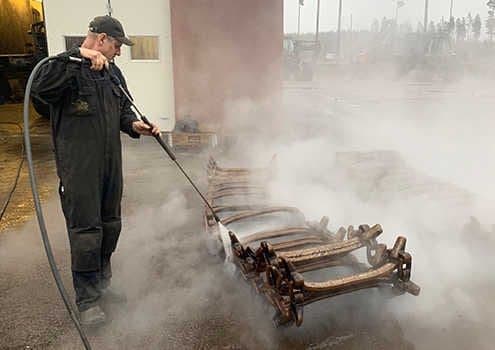
Clean the tracks thoroughly with a pressure washer.
Then leave the tracks at room temperature to dry for at least 24 hours.
Grinding
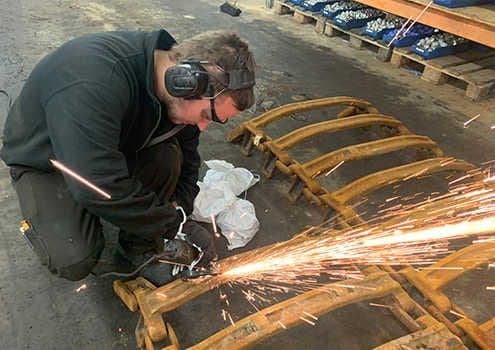
Grind the area where the new stud will go clean of rust and paint.
Never place the new stud closer to the centre of the track plate than the original stud.
We recommend placing the stud just outside the original stud the first time you replace studs. The second time, place it directly over the original stud's position.
Pre-heating
Pre-heat the track plate to 75 °C with propane or acetylene/oxygen.
Welding
Secure the stud with two spot welds, then run a continuous string along both long sides of the stud. Start and finish the string inside the outer edge of the stud. The weld string must never be wider than the stud itself.
Never, under any circumstances, weld across the track plate.
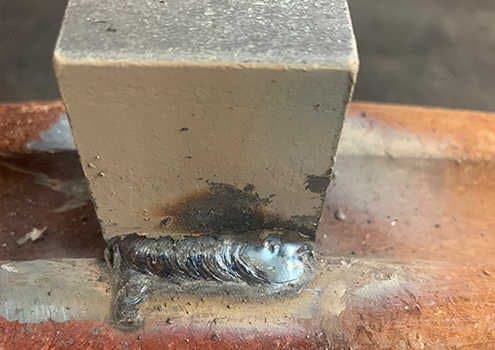
Cooling
Let the weld cool at room temperature, 20–25 °C.
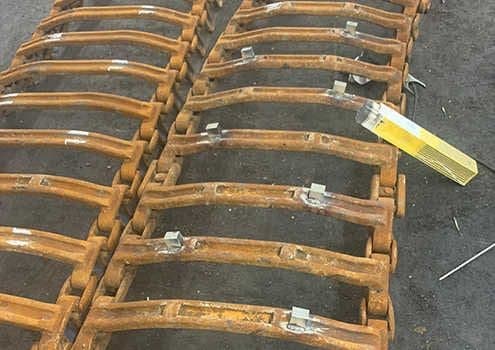
Repeat
Repeat from step 2 on every track plate.
Questions about welding?
Call or email us – we are happy to help with studs, track locks and other spare parts for your tracks.